Industrial Distilling Solutions

Industrial Distillery
Solutions

Comprehensive range of industrial distillery enzymes, fermentation boosters, defoamers, and yeast solutions engineered for commercial molasses and grain distilleries.

Explore Products
Distillery & Fermentation Aids

Advanced Biochemical Solutions for Commercial Distilleries

Praras® is a leading manufacturer of specialty distillery additives and enzymes, offering a comprehensive portfolio designed to optimize starch conversion kinetics, accelerate fermentation cycles, and eliminate processing bottlenecks.

Our FERMAID® line provides substantial improvement in yeast vitality, minimizes diacetyls and volatile acidity, and protects against stress during condensate water reuse. The SOLUBAID® and SACCARAID® ranges deliver rapid high-temperature liquefaction and complete saccharification, maximizing alcohol yield from varied grain and molasses feedstocks.
Molasses Distilleries Grain Distilleries Jet Cooking Systems Recycled Yeast Cultures Condensate Water Reuse Ethanol & Potable Spirits
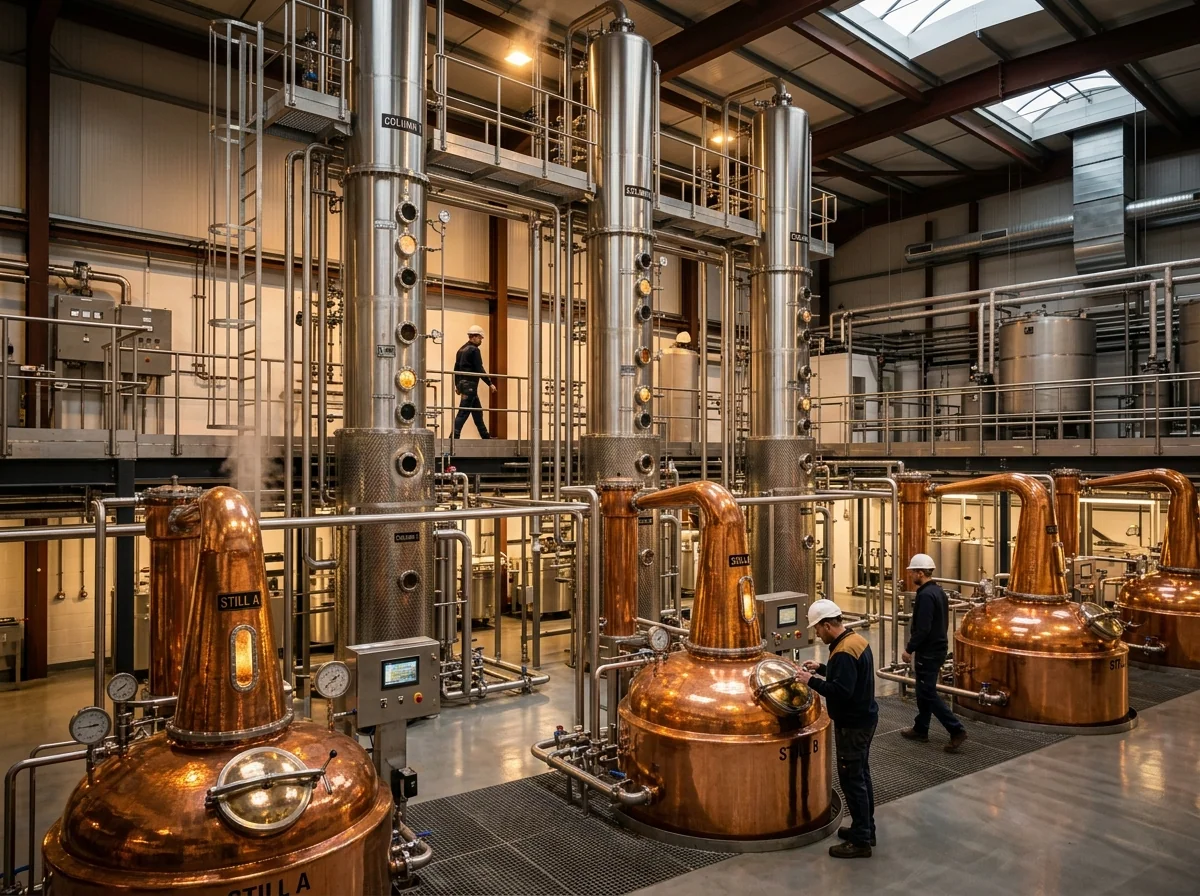
Commercial distillery and spirits processing facility
100+
Distilleries
Served
13+
Distillery Formulations
5
Process Streams Covered
100+
Distilleries Served
15+
Years of Distillery R&D
PROVEN DISTILLERY VALUE

Why Commercial Distilleries Partner with Praras

Tailored biochemical solutions engineered to maximize alcohol yield, accelerate throughput, and ensure unyielding spirit quality.

Higher Alcohol Yield

Maximize fermentable sugar uptake from high-gravity molasses and diverse grain grists, minimizing unfermented residual sugar in spent wash.

104–107°C Jet Cook Stability

Specialized thermostable endo-amylases withstand severe thermal and pressure shear in jet cookers, achieving rapid mash thinning in under 5 minutes.

+10% Working Headspace

Food-grade defoamers and antifoam emulsions suppress vigorous fermenter foam in <10 seconds, eliminating wash overflow and enabling process intensification.

Condensate Water Reuse

Proprietary bio-nutrient complexes neutralize inhibitory volatile acids and osmotic stresses when reusing recycled condensate water in zero liquid discharge plants.

Dextran & Viscosity Breakdown

High-potency fungal dextranases cleave recalcitrant dextran polymers in degraded juice/molasses, preventing heat exchanger fouling and distillation scaling.

FSSAI & Halal Certified

All distillery enzymes and biochemical processing aids are manufactured in FSSC 22000 certified facilities conforming to FSSR 2011 & international standards.

FEEDSTOCK-TO-SPIRIT ARCHITECTURE

Distillery Process Pipeline

Click any stage below to jump directly to its specialized additives and enzymes.

Stage 01
Molasses Wash
Foam suppression, headspace reduction & yield boosters
Stage 02
Viscosity & Dextran
Dextranase enzyme for high-Brix molasses & cane juice
Stage 03
Grain Liquefaction
High-temp jet cooking & rapid alpha-amylase thinning
Stage 04
Saccharification
Complete glucoamylase conversion to D-glucose in SSF
Stage 05
Yeast & Condensate
High-temp active dry yeast & condensate water helper
01

Molasses Fermentation & Defoaming

Rapid foam suppression, headspace minimization, and enzyme-protein yield optimization for molasses wash

5 Formulations
AIDFERM AFL0120®
Molasses
Where Used: Molasses & Grain Fermenters
Activity: Defoam Time <10s @ 0.1–5.0 ml
Nature: Food-Grade Silicone Emulsion
Benefits: Instant foam suppression, disperses efficiently, prevents wash overflow
📏 1–3 g/HL Wort (10–30 ppm)
Details →
FERMAID AF®
Molasses
Where Used: Fermenters & Yeast Scaling Media
Activity: Polydimethylsiloxane Base
Nature: Fermentation Antifoam
Benefits: Increases tank capacity by 10% via headspace reduction; safe for recycled yeast
📏 1–3 g/HL Wort (10–30 ppm)
Details →
FERMAID PLUS®
Molasses
Where Used: High-Gravity Molasses Fermentation
Activity: Amylase NLT 100,000 IU/g | Protein NLT 20%
Nature: Amylase Enzyme & Bio-Protein Complex
Benefits: Maximizes alcohol yield, accelerates yeast metabolism & minimizes by-products
📏 3–5 ppm Wash (10–15 g/MT Molasses)
Details →
FERMAID P®
Molasses
Where Used: Molasses Wash Fermentation
Activity: Amylase NLT 80,000 IU/g | Protein NLT 10%
Nature: Amylase Enzyme & Bio-Nutrient Complex
Benefits: Two-stage booster reducing volatile acidity and unfermented residual sugars
📏 5–8 ppm Wash (15–24 g/MT Molasses)
Details →
SOLUBAID S®
Molasses
Where Used: Molasses Wash & Cane Juice
Activity: Amylase NLT 8,000 IU/mg | SG 1.10–1.20
Nature: Bacterial Alpha-Amylase Liquid
Benefits: Hydrolyzes starch in molasses wash, reducing viscosity & boosting alcohol conversion
📏 5–10 g/Ton Cane (5–8 g/m³ Wash)
Details →
02

Viscosity & Dextran Control

Hydrolyzes complex dextrans to eliminate process viscosity, pan scaling, and distillation inefficiencies

1 Formulation
SOLUBAID DXP®
Dextranase
Where Used: Contaminated Cane Juice & Molasses Wash
Activity: Dextranase NLT 100,000 IU/g
Nature: Fungal Dextranase Enzyme Formulation
Benefits: Hydrolyzes dextrans into smaller oligosaccharides, reducing viscosity, foaming & sugar loss
📏 4–8 ppm Wash (1–3 ppm on Juice)
Details →
03

Grain Liquefaction & Jet Cooking

High-temperature endo- and exo-amylases engineered to withstand jet cooking temperatures (104–107°C) and pressure shear

3 Formulations
SOLUBAID G®
Jet Cooker
Where Used: Grain Jet Cooking (104–107°C)
Activity: Bacillus licheniformis | SG 1.10–1.20
Nature: High-Temp Liquid Endo-Amylase
Benefits: Rapid α-1,4 bond cleavage under high pressure (50–70 psi), fast mash viscosity drop & anti-retrogradation
📏 0.60–0.80 kg/Ton Dry Starch (1–3 g/HL)
Details →
SOLUBAID AS®
Jet Cooking
Where Used: High-Temp Grain Slurry Jet Cooking
Activity: Amylase NLT 8,000 IU/g | SG 1.10–1.20
Nature: Endo-Amylase Liquefaction Booster
Benefits: Improves starch solubilization efficiency at high temperatures across varied grain feedstocks
📏 0.60–0.80 kg/Ton Dry Starch
Details →
SACCARAID B®
Mash Tun
Where Used: Grain Cooking & Mash Tun (85–95°C)
Activity: Exo-Amylase Activity NLT 80,000 IU/g
Nature: Thermostable Exo-Amylase Liquid
Benefits: Rapid reduction in cooked starch paste viscosity, preparing slurry for complete downstream saccharification
📏 5–10 g/Ton Cane (0.4–0.6 kg/T Starch)
Details →
04

Grain Saccharification & SSF

High-purity glucoamylases for complete dextrin-to-glucose conversion in Simultaneous Saccharification and Fermentation

2 Formulations
SACCARAID G®
Glucoamylase
Where Used: Grain Mash Saccharification & SSF
Activity: Glucoamylase NLT 80,000 IU/g
Nature: High-Purity Exo-Amylase Liquid
Benefits: Complete conversion of liquefying dextrins to D-glucose (48–60% DE) at 58–60°C, maximizing ethanol recovery
📏 0.65–0.85 kg/Ton Dry Starch (1–3 ppm)
Details →
SACCARAID GL®
Complex Amylase
Where Used: Grain Liquefaction & Saccharification
Activity: Amylase NLT 80,000 IU/g
Nature: Concentrated Amylolytic Complex
Benefits: Broad-temperature amylolytic action (30–45°C) accelerating starch breakdown into fermentable sugars
📏 0.4–0.8 L/Ton Starch (5–6 kg/Lakh L)
Details →
05

Yeast & Condensate Water Reuse

Thermo-tolerant active dry yeast and bio-nutrient helpers engineered to sustain fermentation vigor under thermal and recycled water stress

2 Formulations
GISTADD-HST®
Active Dry Yeast
Where Used: High-Temp Grain & Molasses Fermenters
Activity: Live Cells NLT 80–90% | Count NLT 1x10⁸ cfu/g
Nature: Thermo-Tolerant Active Dry Yeast
Benefits: Fast, robust fermentation up to 40°C heat stress; maintains high efficiency with recycled condensate water
📏 0.4–0.6 kg/Ton Starch (5–6 kg/Lakh L)
Details →
FERMAID PI®
Condensate Water
Where Used: Recycled Condensate Water Wash
Activity: Amylase NLT 100,000 IU/g | Protein NLT 10%
Nature: Condensate Water Fermentation Helper
Benefits: Neutralizes inhibitory volatile acids & osmotic stress during use and reuse of condensate water
📏 4–8 ppm Wash (10–15 g/MT Molasses)
Details →
FEEDSTOCK & DISTILLERY CAPABILITY

Engineered for Diverse Distillery Configurations

Whether operating grain jet-cooking streams, molasses batch plants, or zero-liquid discharge setups, our biochemical formulations deliver tailored performance.

Molasses Distilleries

Cane & Beet

Optimizes high-gravity molasses washes by suppressing volatile acidity, controlling krausen foam in <10s, and boosting alcohol yield per MT of raw molasses.

AIDFERM AFL0120® FERMAID AF® FERMAID PLUS® FERMAID P® SOLUBAID S®

Grain Distilleries

Corn / Rice / Wheat

Withstands extreme jet cooker thermal shock (104–107°C / 50–70 psi) for rapid liquefaction and complete glucoamylase saccharification in SSF fermenters.

SOLUBAID G® SOLUBAID AS® SACCARAID B® SACCARAID G® SACCARAID GL®

ZLD & Condensate Reuse

Eco-Efficiency

Protects yeast viability in Zero Liquid Discharge (ZLD) plants where condensate water recycling introduces thermal and volatile chemical osmotic stresses.

GISTADD-HST® FERMAID PI® SOLUBAID DXP®
COMMERCIAL DISTILLERY PARTNERSHIP

Optimize Your Distillery Yield & Throughput

Connect with our senior biochemical specialists for plant-level enzyme trials, custom dosage recommendations, and technical support.

Contact Technical Team